Section 4- roll reducing and end finishing
After filled the tubes well, reduce the tubes to increase the density, equipment need as below:
(1) 2 sets Auto feeder with withstand test (item: SL-1500PLC), Φ10 and Φ9.5 each one set, the qualified tubes will be automatically sent to the reducing machine to reduce, the unqualified tubes will be selected to other position of the machine and waiting to be arranged.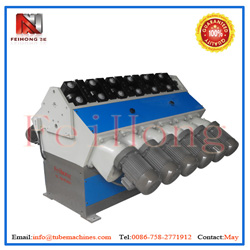
(2) 2 sets 12 pairs roll reducing machine (item: SG12B), 1 set Φ10- Φ8.5 and 1 set Φ9.5-Φ8. We can choose tungsten carbidge hard alloy rolls for the moulds.
(3) 2 sets Straightening Machine (TB-12), to make packing step smoothly, add a straightening machine at the connection of roll reducing machine.
(4) 2 sets Auto roll turnign machine (CG50-1500 PLC), after reduced the tubes, remove the spare part of the tube, let the terminal pins exposing. Need one set for Φ8.5, one set for Φ8.
(5) 2 sets Automatic Digging Powder Machine. Dig the MGO powder at the ends of the pipe, to get ready for installation of ceramic plug and sealing. The machine is similar with roll turning machine, only the cutters different.
(6) 1 set Rod Cutting Machine, Using electric punch machine mould, cut of the excess terminal pins.
Section 5 - hardware
(1). 1 set Taper Temperature Tube Machine, Reduce the front part of the tube to be cone shape to weld.
(2) 1 set Flat Temperature Tube Machine.
(3) Stainless steel flange, use punch machine to processing, included stretching, punching 4 steps. The Punch machine choose 2 styles, that is 63 tons and 40 tons.
QTY: 60 ton one set, 40 ton 3 sets. |
 tube.machines
.jpg)

.jpg)


